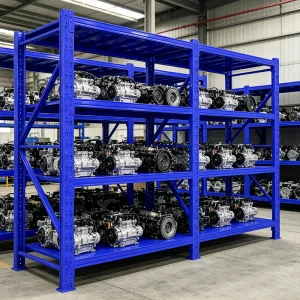
The modern global supply chain ecosystem is undergoing an unprecedented transformation driven by the exponential growth of e-commerce, omnichannel retail, and automated fulfillment centers. In this high-velocity environment, warehouse space optimization is no longer just a real estate consideration; it is a critical competitive advantage. Industrial warehouse shelving manufacturers must engineer structural storage assets that maximize vertical cubic capacity while ensuring uncompromising operator safety and structural longevity.
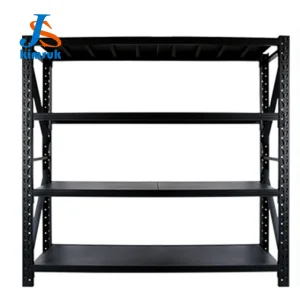
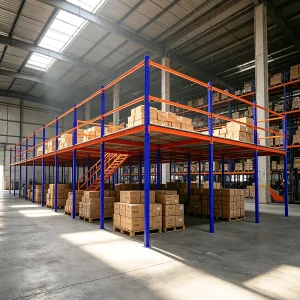
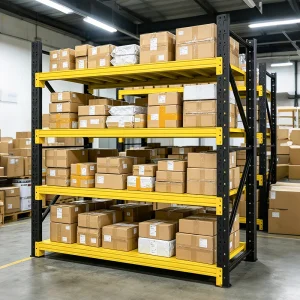
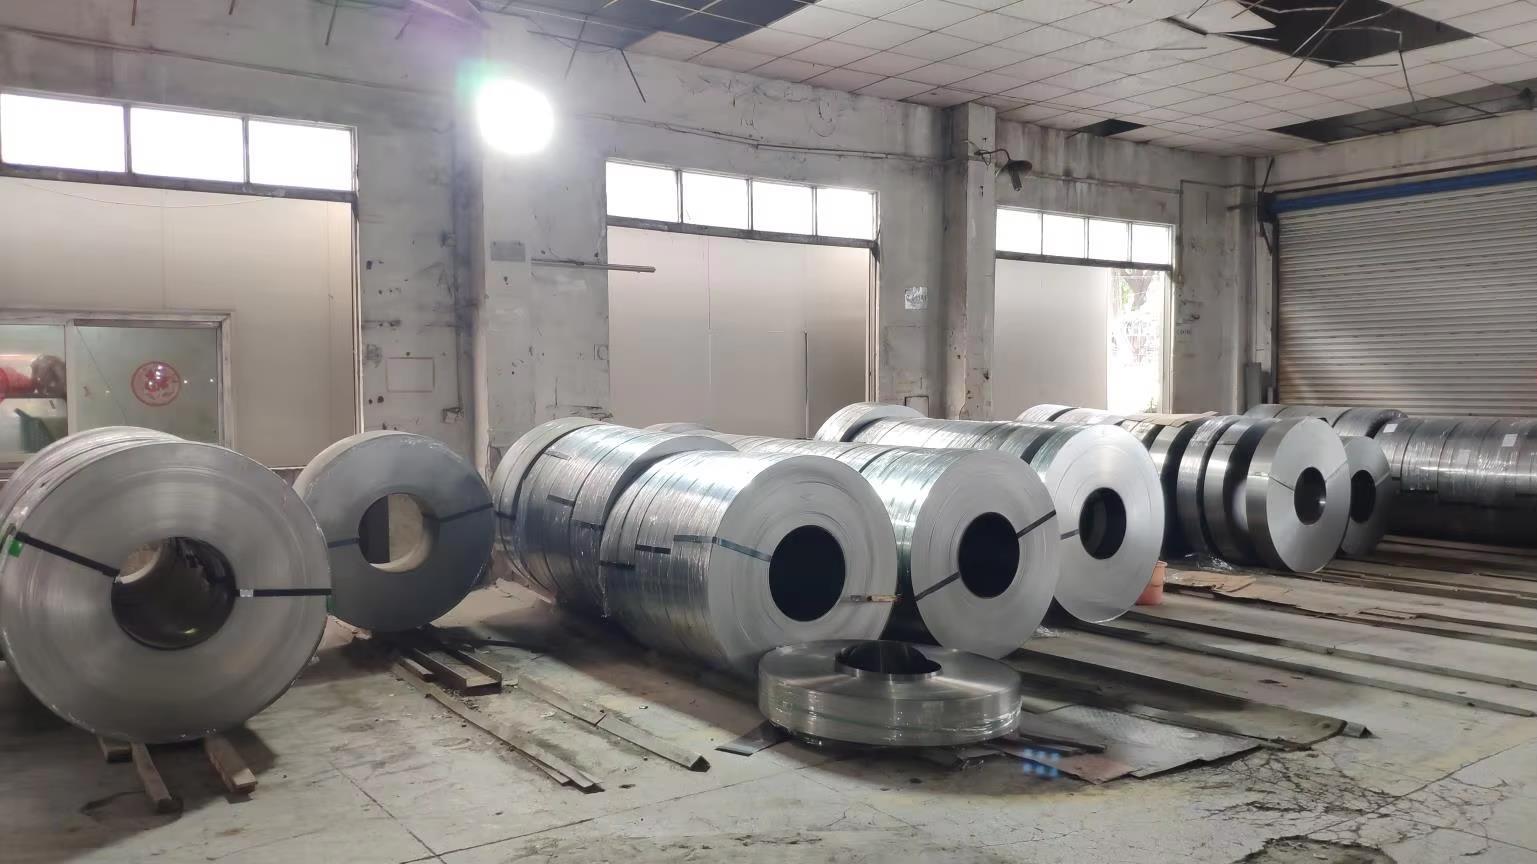
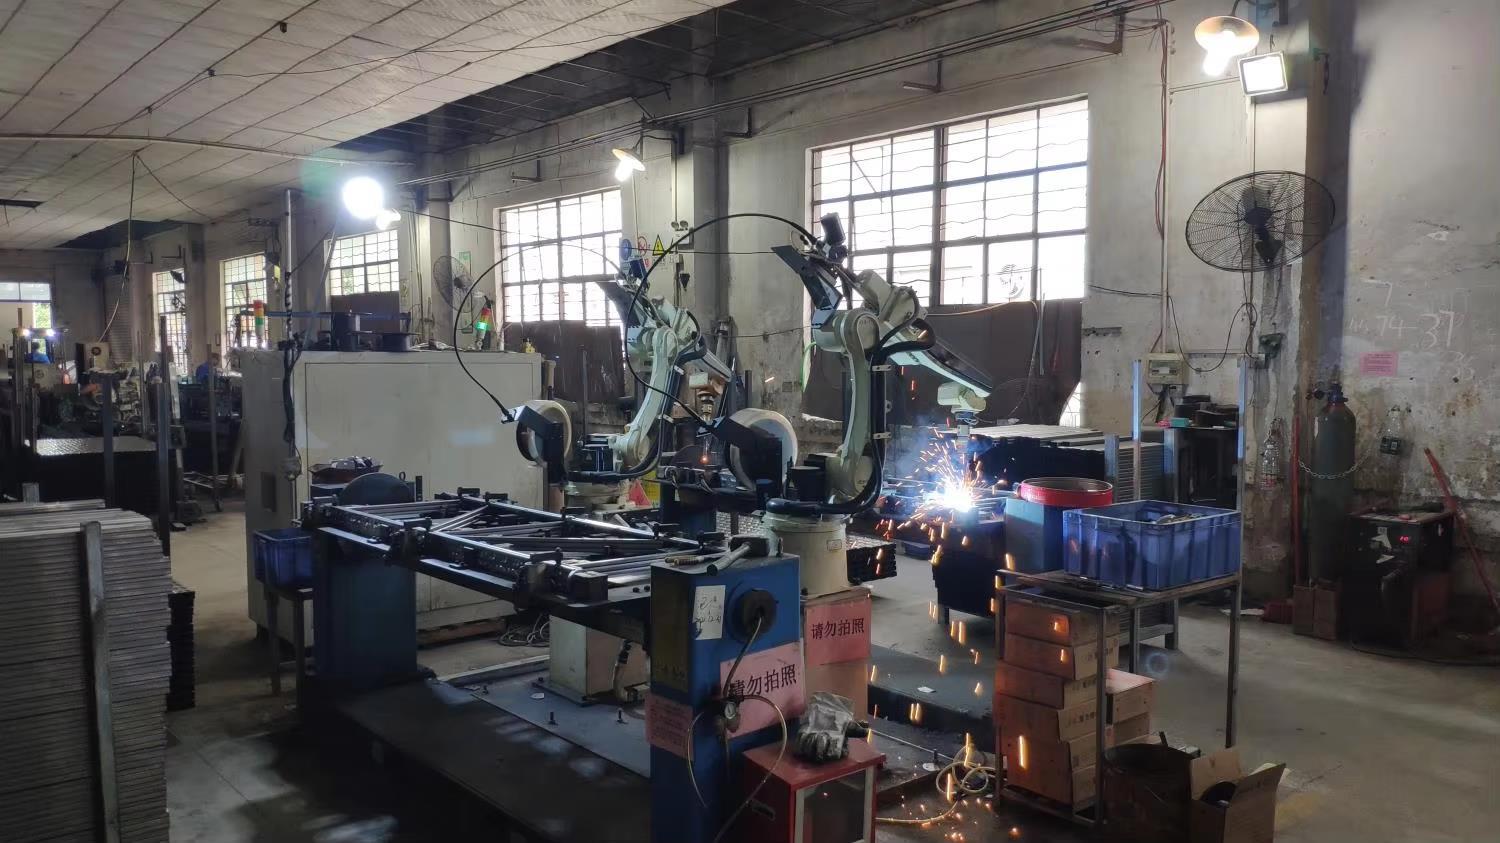
As international logistics hubs face soaring land and construction costs, enterprise procurement managers are increasingly prioritizing high-density shelving structures, multi-tier mezzanine floor systems, and customizable heavy-duty cantilever or pallet racking systems. The integration of precision-rolled cold-rolled steel, automated robotic welding, and stringent quality protocols guarantees that modern storage infrastructure can withstand rigorous day-to-day handling in demanding industrial environments.
Global enterprise buyers, ranging from third-party logistics (3PL) providers to automotive components distributors and cold-chain operators, demand rigorous compliance standards. CE certification, seismic load engineering, and customized corrosion-resistant powder coatings are now baseline expectations for tier-one international supply chains.
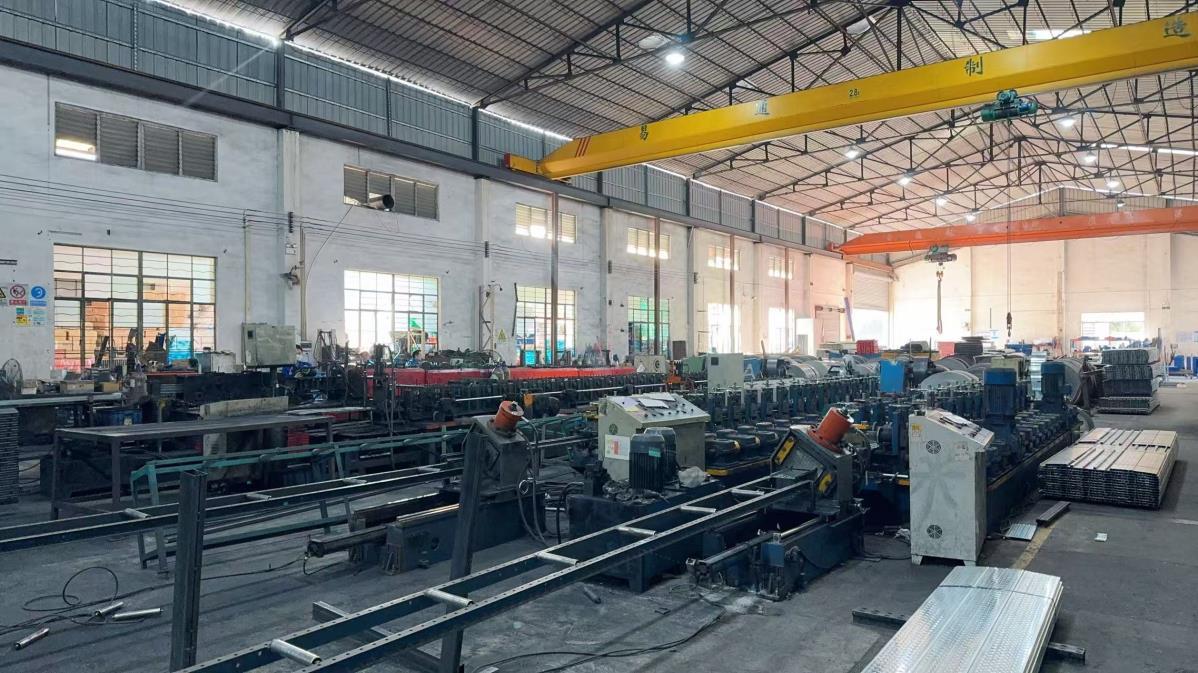
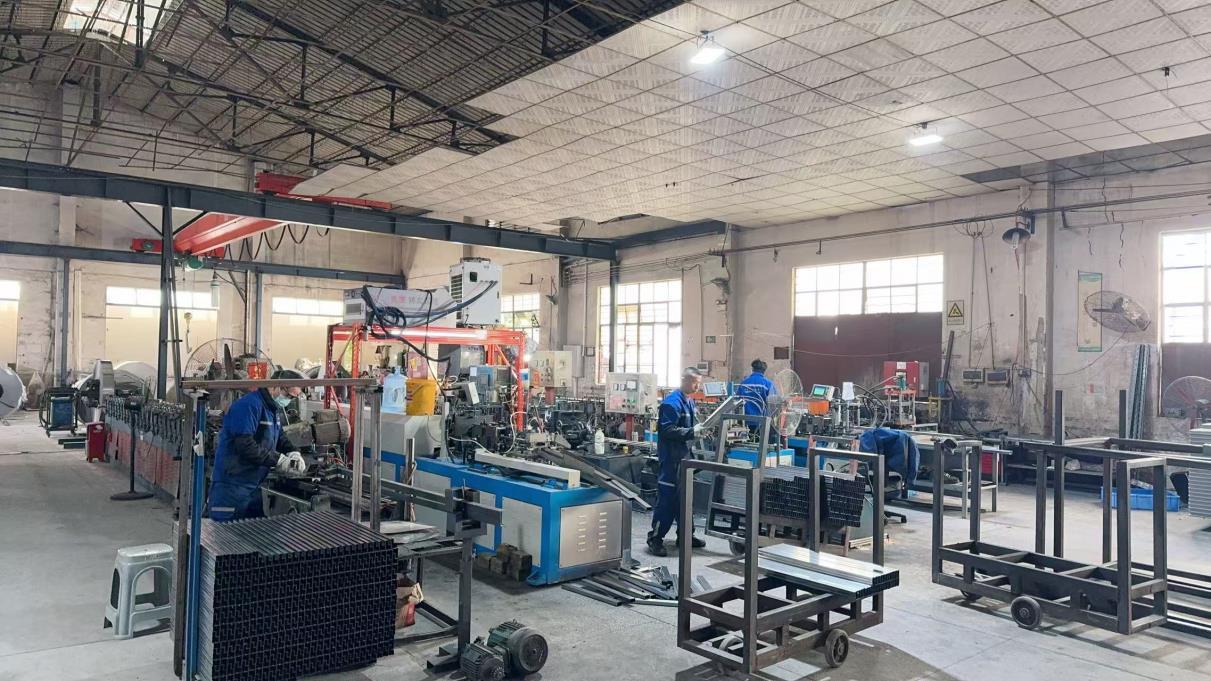
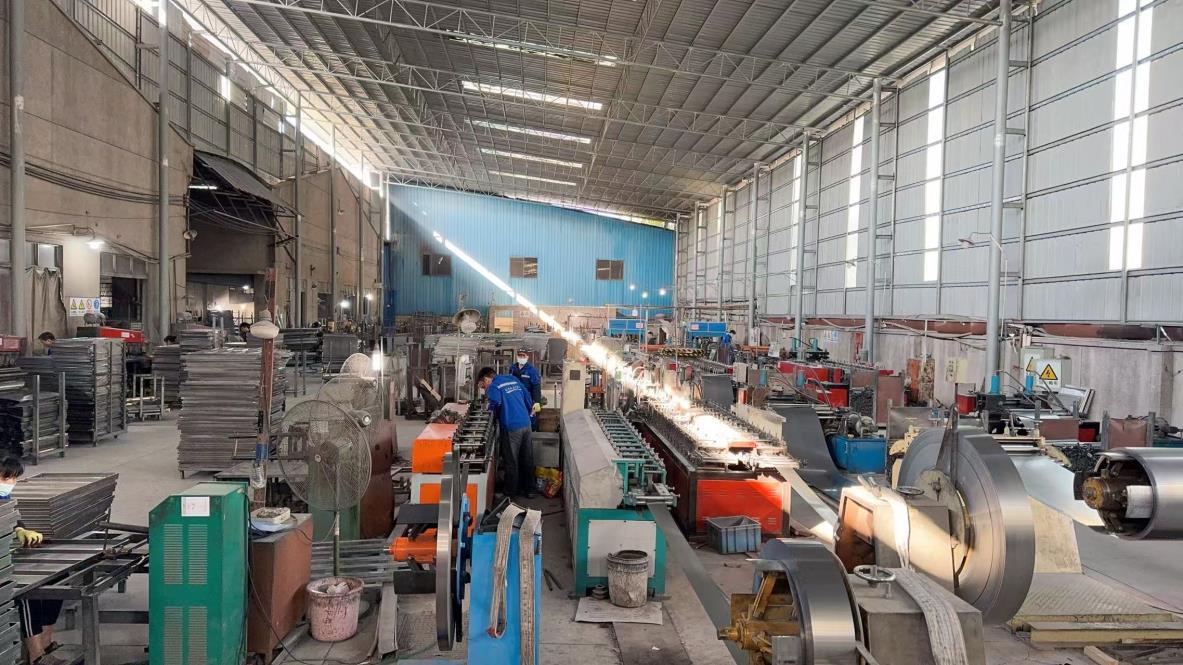
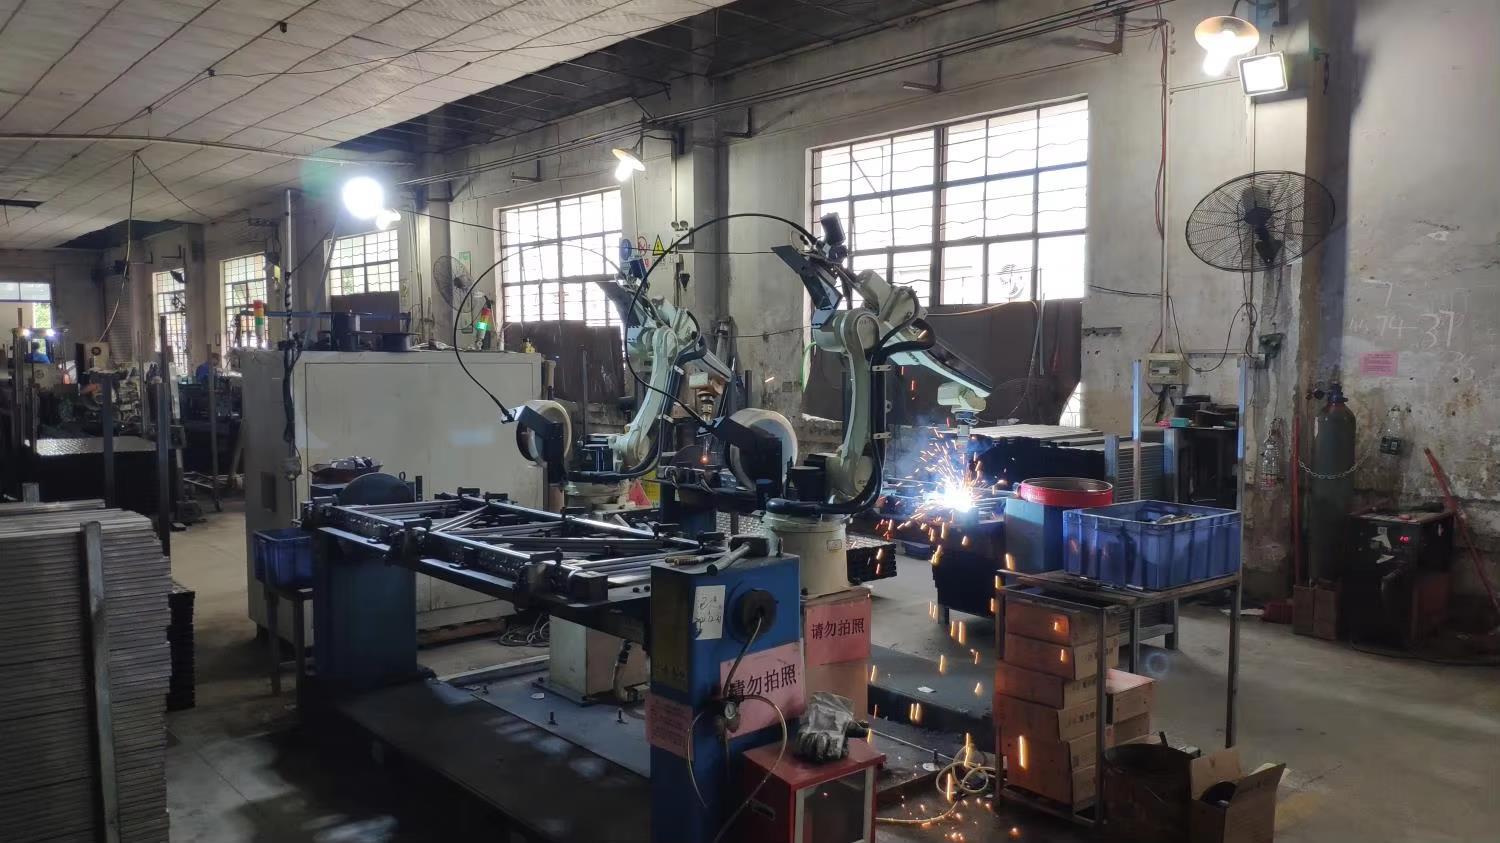
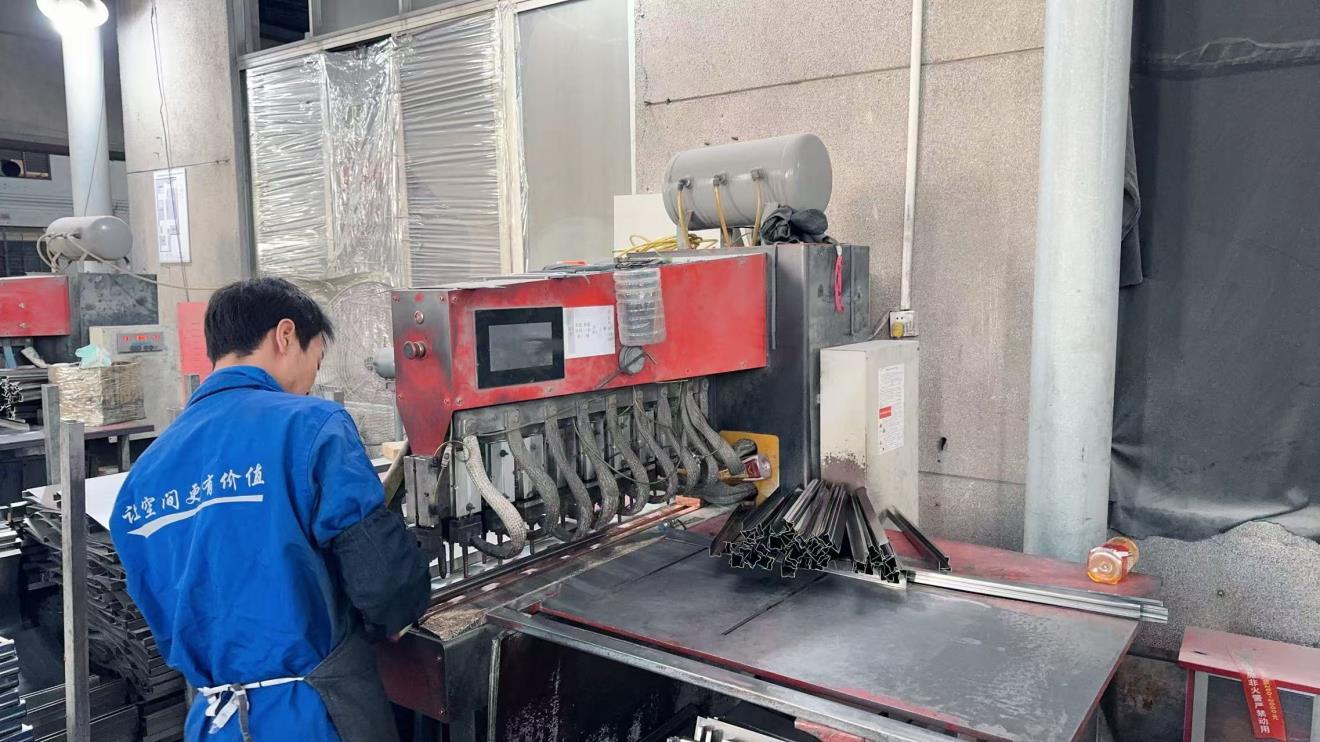
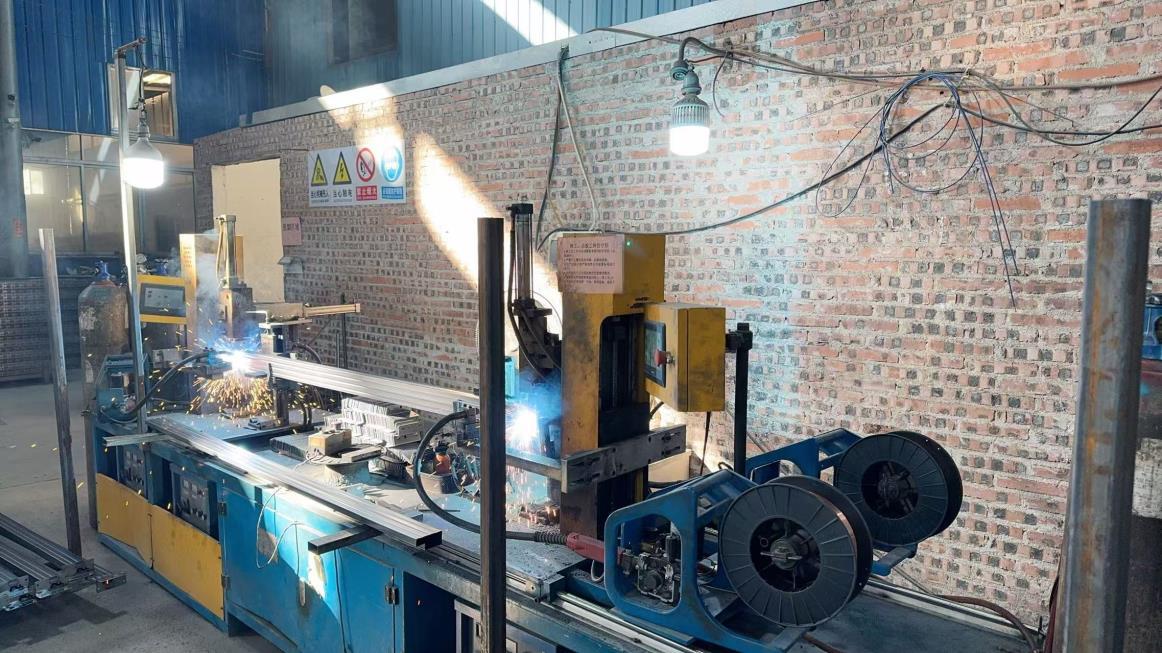
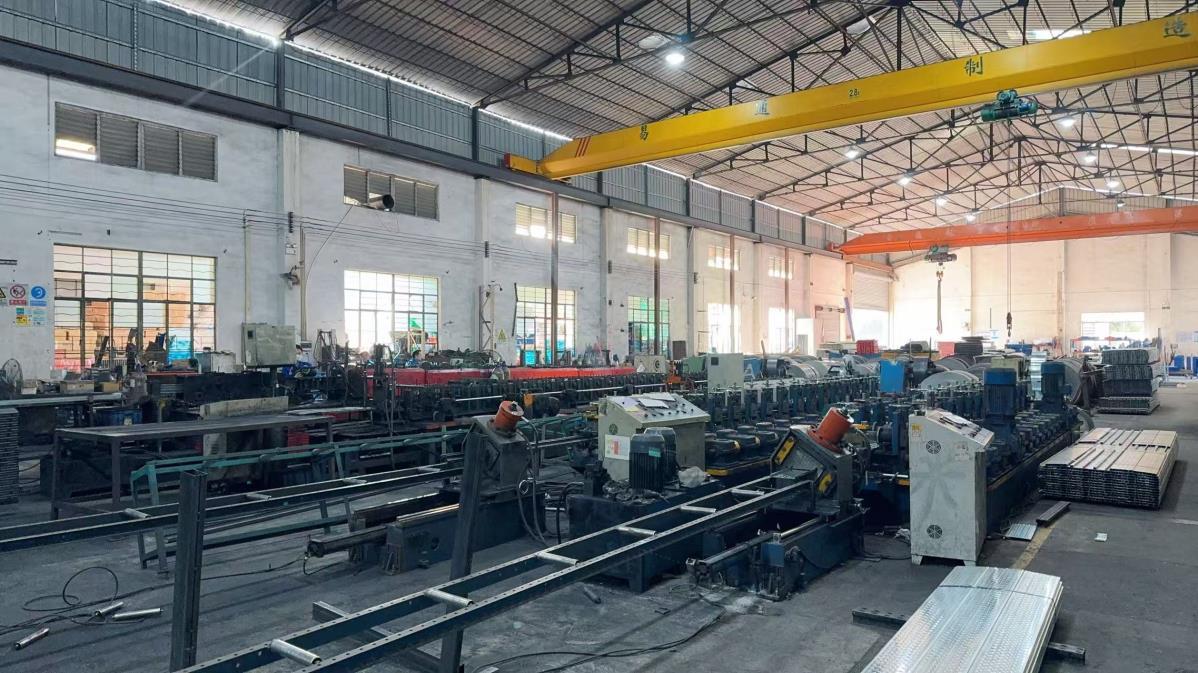
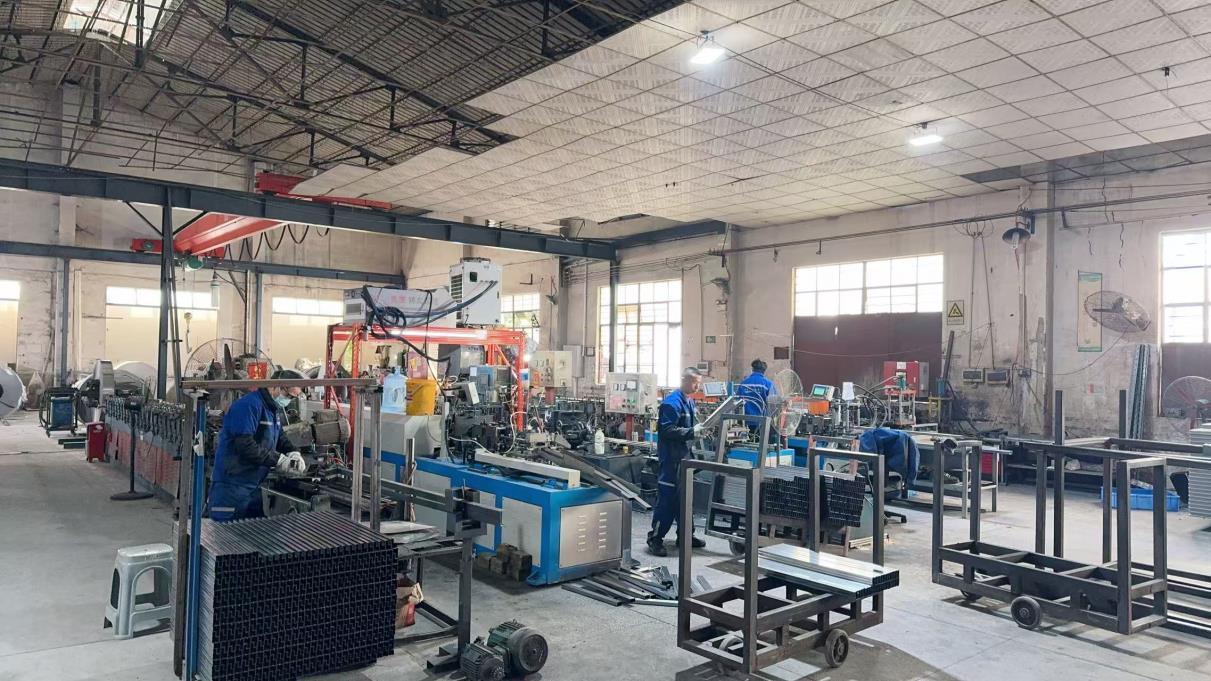
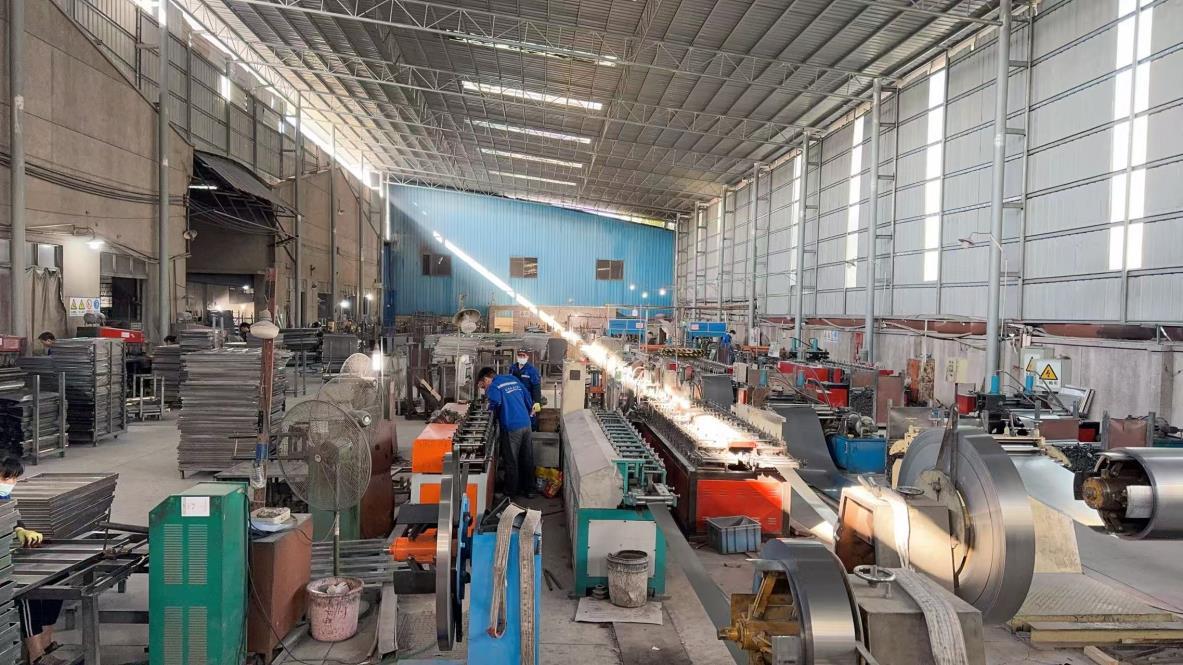
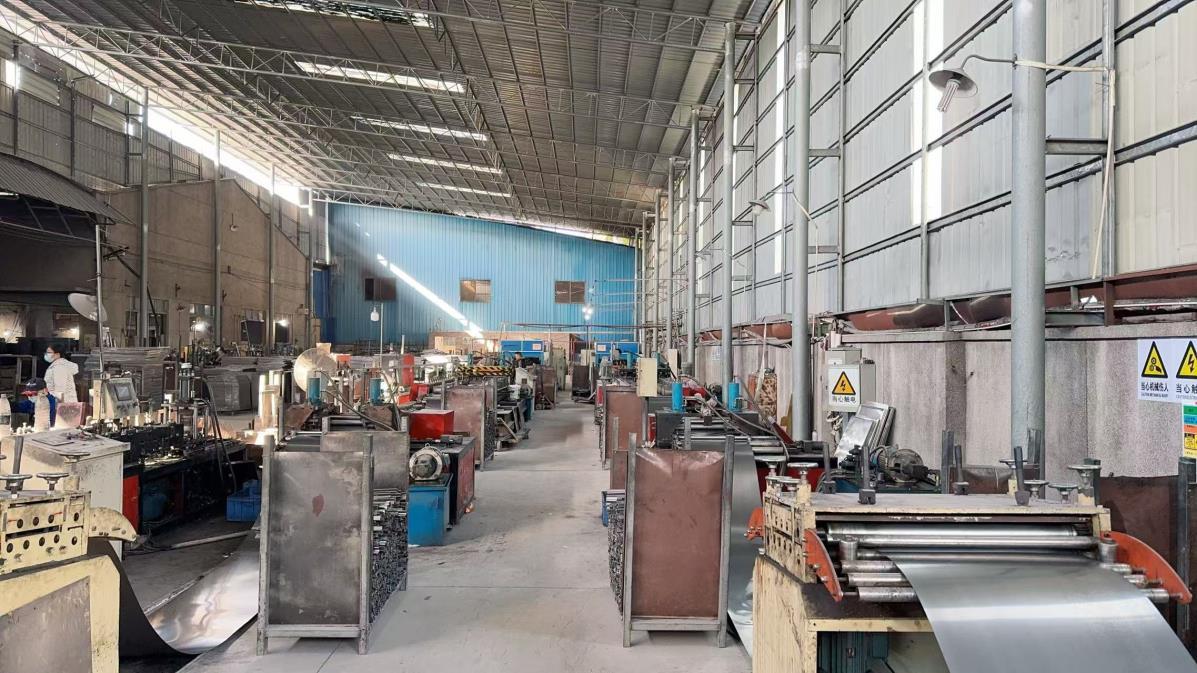
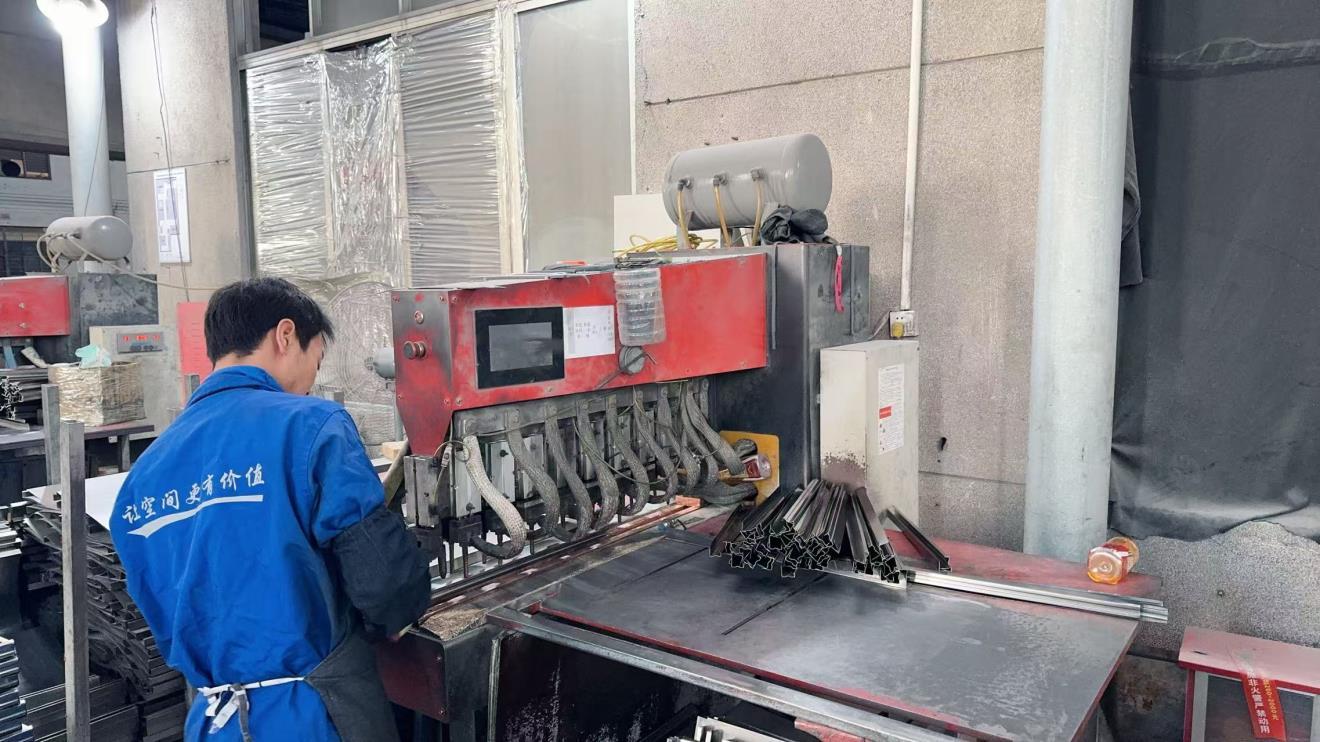
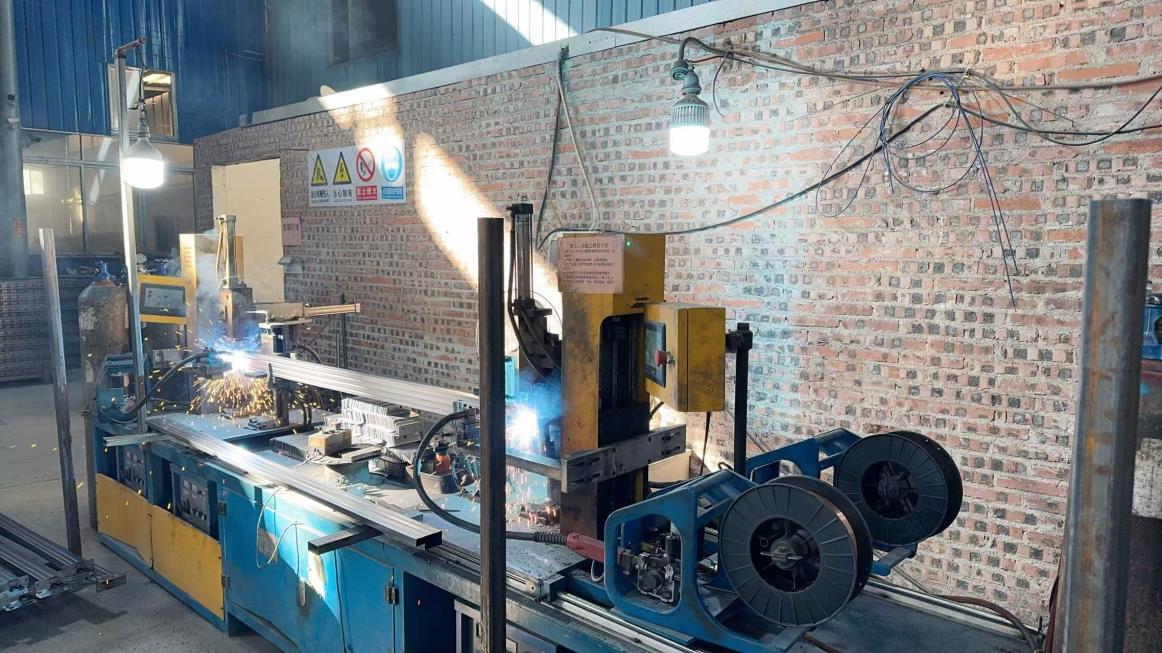
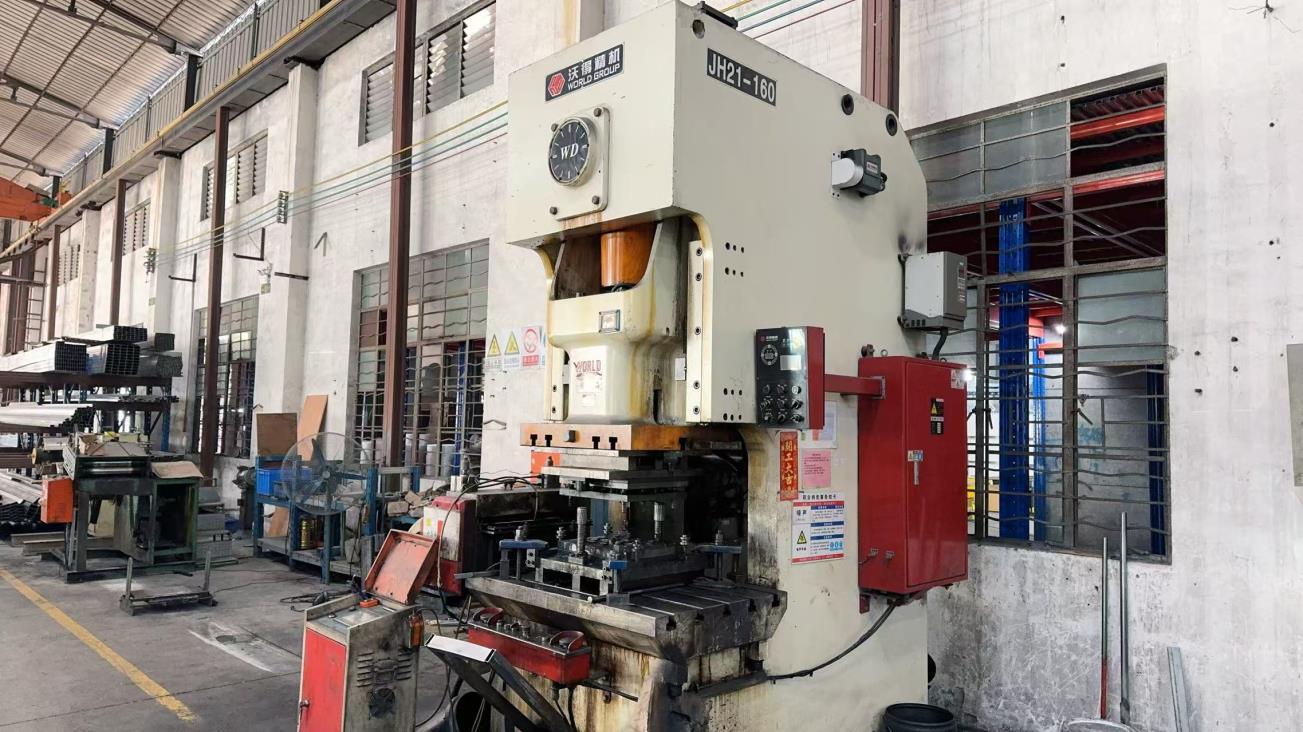
Chinese manufacturing excellence has transitioned into Industry 4.0 standards. Utilizing automated laser cutting lines, robotic welding arms, and computer-controlled stamping machinery ensures uniform structural integrity, micron-level precision, and fast, reliable delivery schedules for global importers.
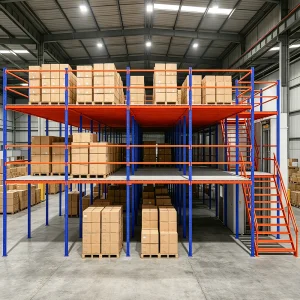
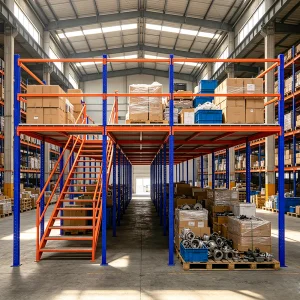
From heavy-duty cold room pallet racks engineered to withstand sub-zero temperatures, to multi-level mezzanine systems doubling retail storage footprints, our shelving configurations are tailor-made to solve distinct spatial challenges across diverse commercial sectors.
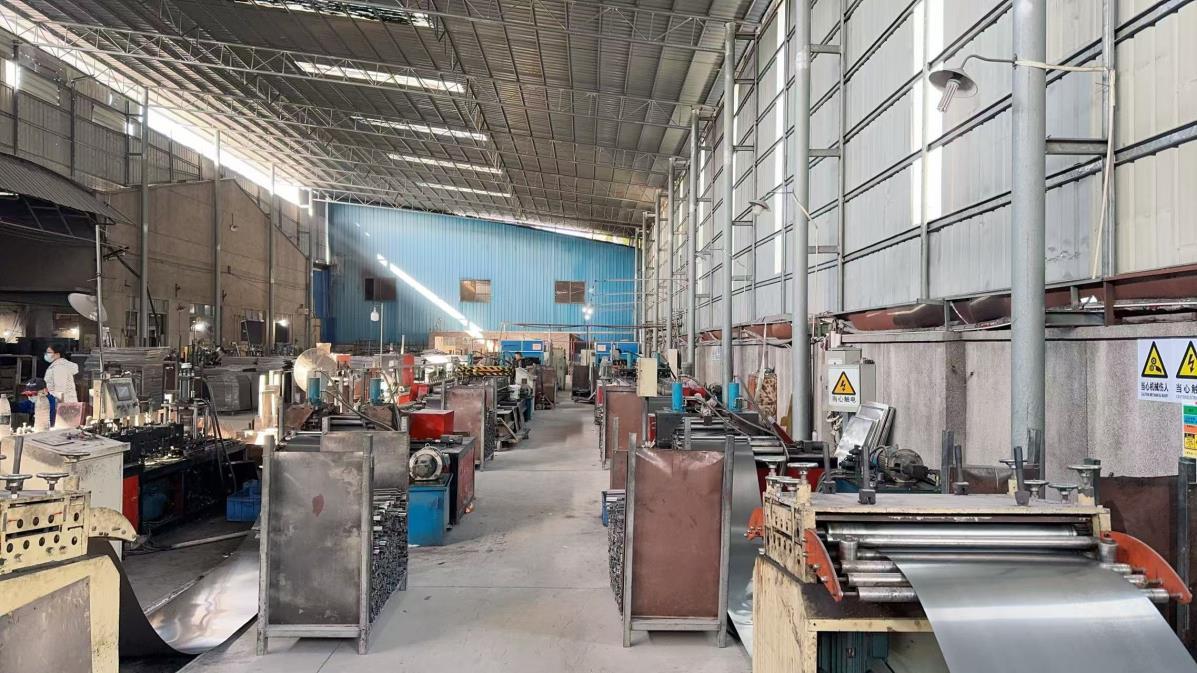
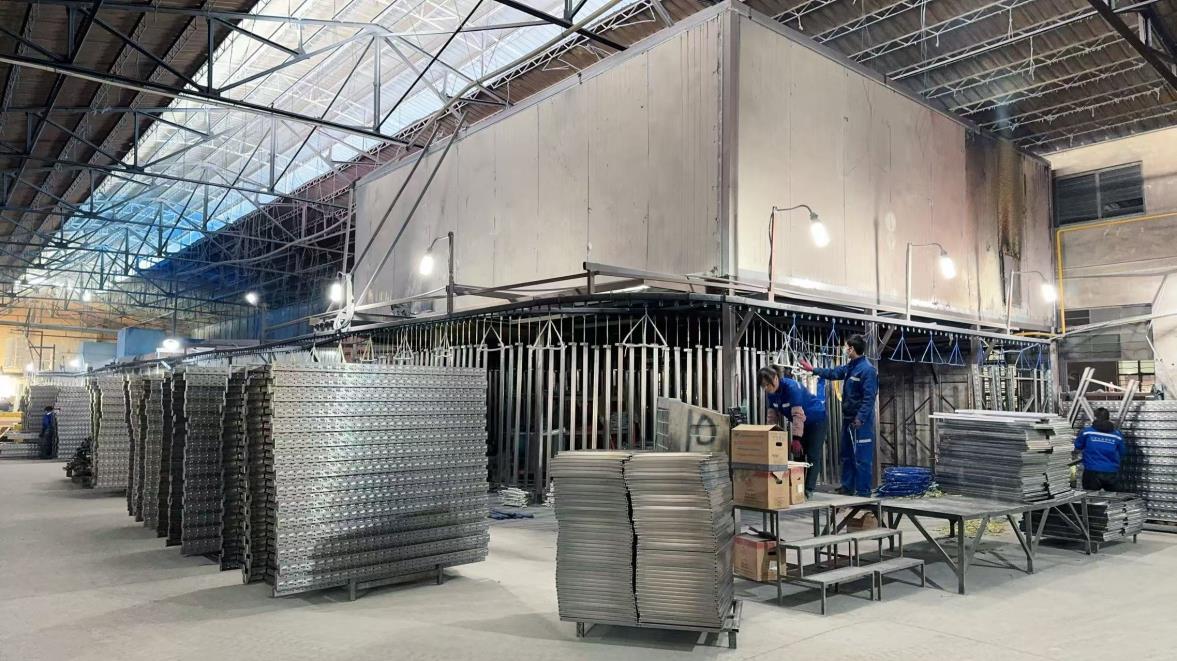
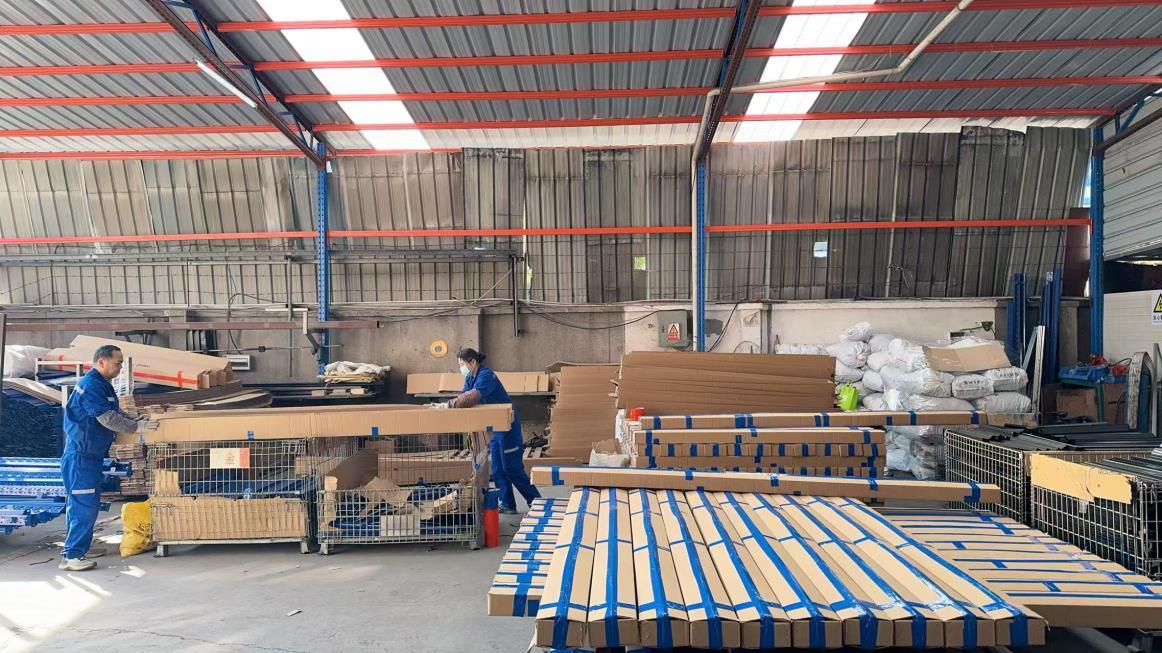
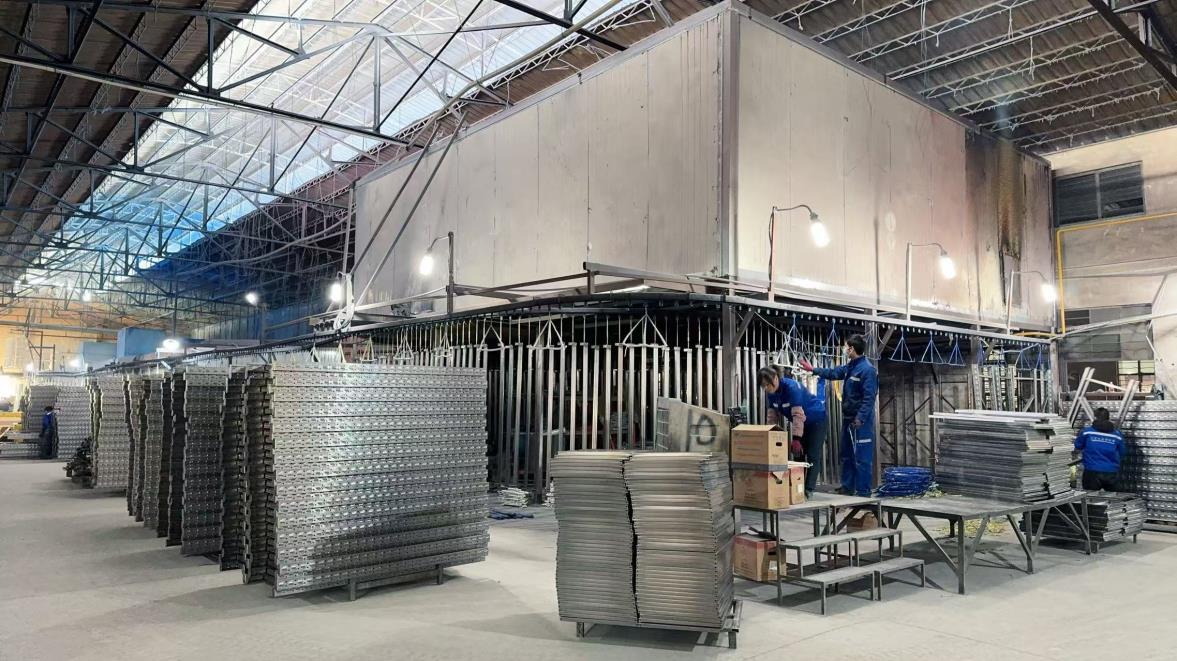
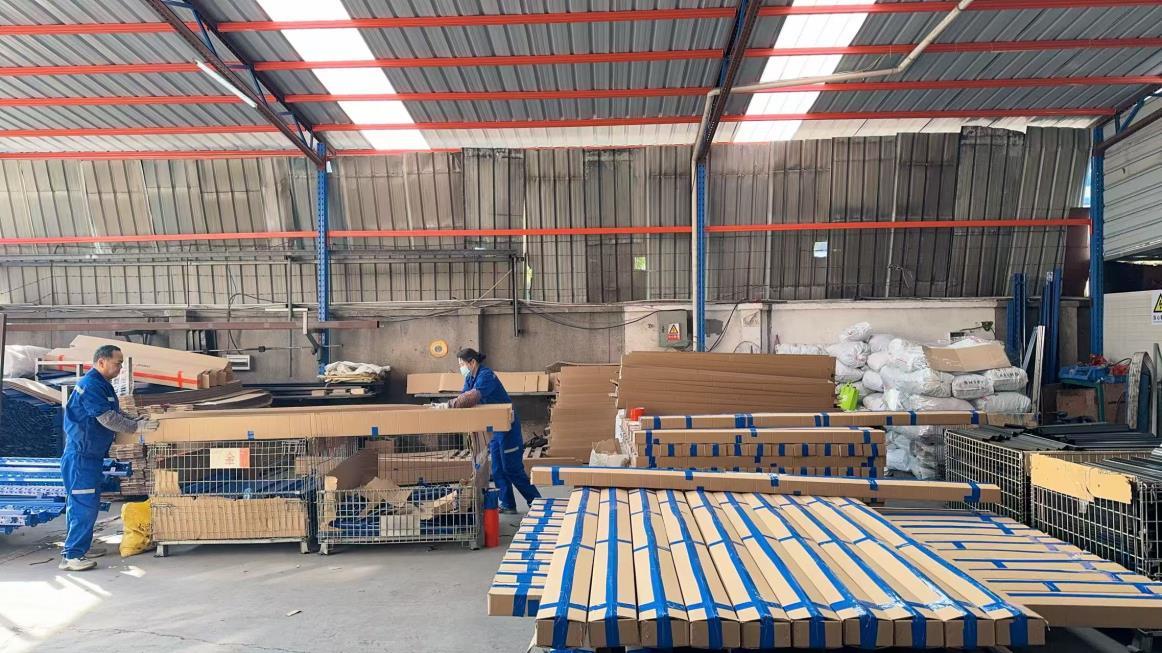
Established in 2015, Dongguan Kimsuk Shelves Co., Ltd. is a leading manufacturer specializing in the design, engineering, and production of heavy-duty industrial shelving and warehouse storage systems. Operating from a modern production facility spanning 32,000 square meters, we have grown into a trusted global supply chain partner with 11 years of industry expertise and 8 years of direct international export experience. Driven by robust manufacturing capability, our annual export revenue reaches $18 million, serving clients across key international markets, including North America, Europe, Southeast Asia, and the Middle East.
Quality and precise engineering are at the core of our operations. We maintain a strict Quality Assurance protocol supported by a dedicated team of 35 QA/QC inspectors. Our comprehensive product inspection methods combine automated non-destructive testing, raw material tensile testing, load-bearing stress evaluations, and precision powder-coating thickness measurements. Supported by an extensive network of over 850 verified supply chain partners, we consistently deliver reliable, high-integrity racking systems to a diverse client portfolio, ranging from large-scale logistics hubs and third-party logistics (3PL) providers to industrial manufacturing facilities and commercial retail distributors.
Innovation drives our growth. Our in-house R&D team consists of 18 senior structural and engineering specialists capable of delivering full OEM/ODM custom solutions. From tailored rack dimensions and heavy load capacities to specialized seismic-resistant structures and anti-corrosion surface finishes, we turn complex warehousing requirements into optimal designs. Demonstrating our continuous drive for innovation, we successfully developed and launched 120 new product models and modular storage enhancements last year alone. At Dongguan Kimsuk Shelves Co., Ltd., we remain committed to maximizing warehouse space efficiency and delivering long-term value to our global partners.
 Kimsuk Steel